Silicone Valve
custom NBR valve
Food-contact-safe NBR raw material
MOQ: 50,000 pcs/lot
DESCRIPTION
Specification
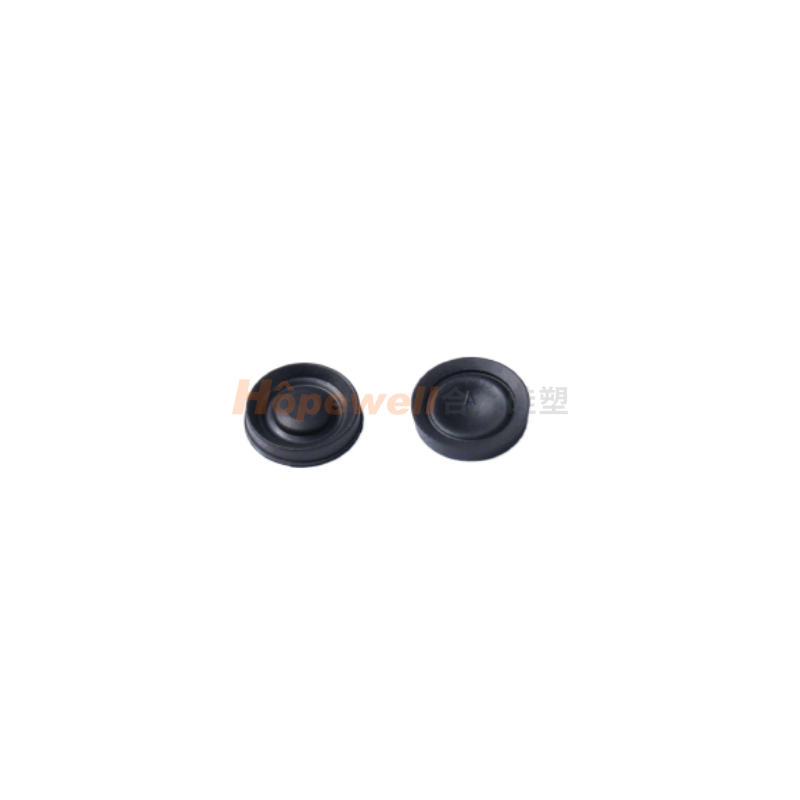
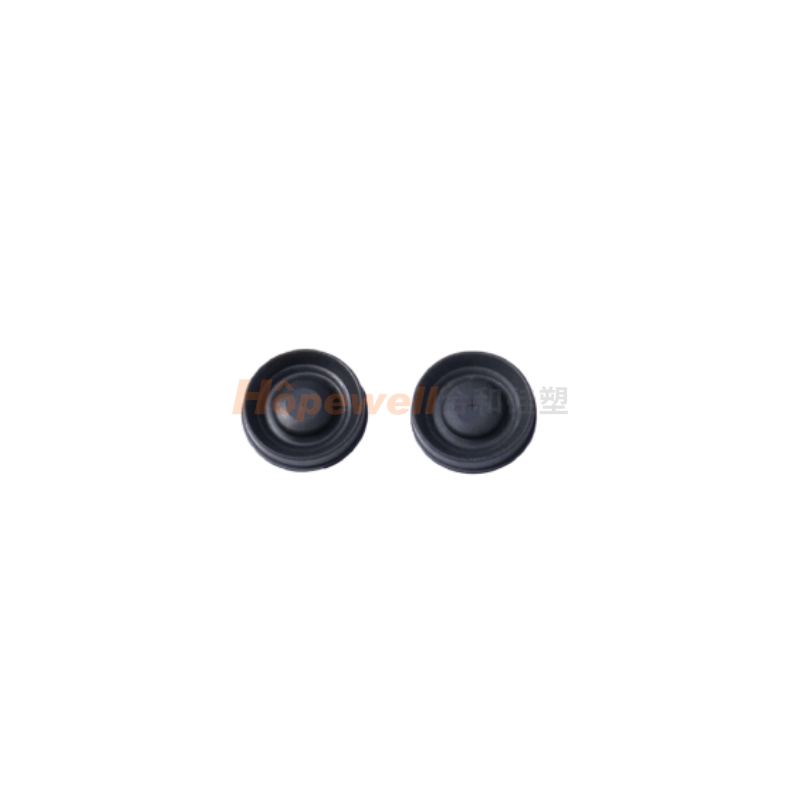
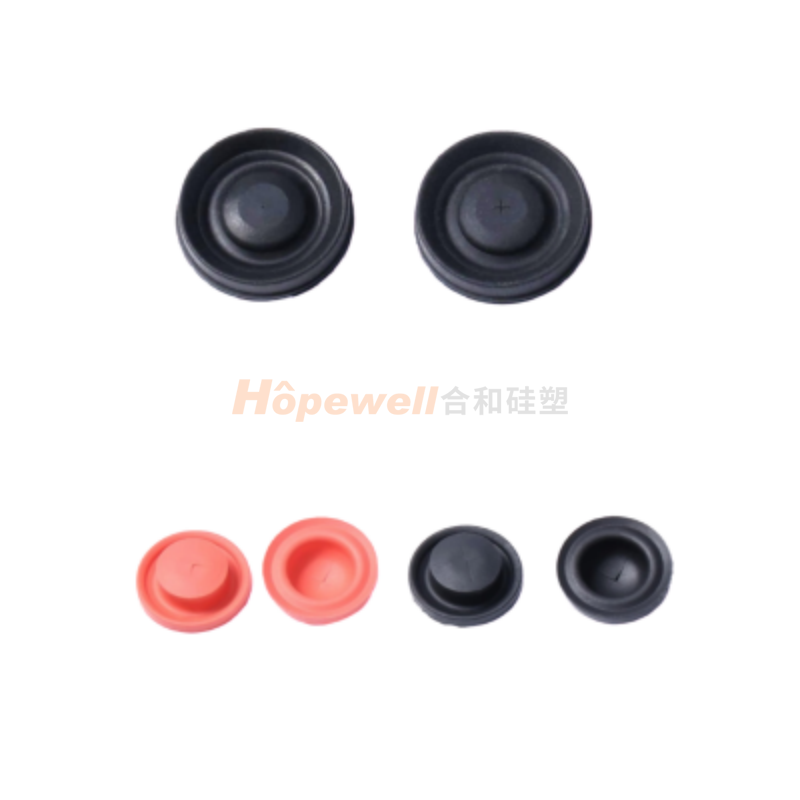
Hopewell's NBR rubber valve (nitrile butadiene rubber valve) is specially developed for cosmetic dispensing packaging, providing precise flow control and excellent sealing performance for oil-based skincare and beauty products.
Made from high-performance nitrile rubber (NBR), this valve offers superior resistance against oils, greases, solvents, and hydrocarbon-based ingredients commonly found in cosmetic formulations. Unlike silicone valves, which may swell or lose elasticity when exposed to oils, NBR valves maintain stable performance and reliable sealing even with oil-based products.
The self-sealing design allows smooth product extrusion when the bottle is squeezed and automatically closes after dispensing, helping prevent air backflow, contamination, and product waste.
With excellent oil resistance, mechanical strength, and durability, our NBR rubber valve is an ideal dispensing solution for cosmetic brands, packaging manufacturers, and personal care product suppliers.
Product Type | custom NBR valve |
Outer Diameter | customize |
Hardness | customize |
Slit Cut Type | customize |
Slit Cut Size | customize |
Material | food grade NBR |
Color | customize |
Production Process | injection molding |
Application | for cosmetic dispensing |
MOQ | 50,000 pcs/lot |
The one-way NBR valve (nitrile rubber valve) is widely used in cosmetic and personal care packaging applications where oil or solvent content is high, including:
Sunscreen cream
Essential oils and serums
Moisturizing lotion
Anti-aging cream
Eye cream
Facial cleanser
Foundation
BB cream
Makeup primer
Liquid concealer
Cosmetic gels
Oil-based skincare products
Cosmetic emulsions
Hair treatment products
Industrial lubricants and cleaning agents
The NBR rubber valve can be customized according to different product viscosities, dispensing requirements, and packaging structures.
Product Information
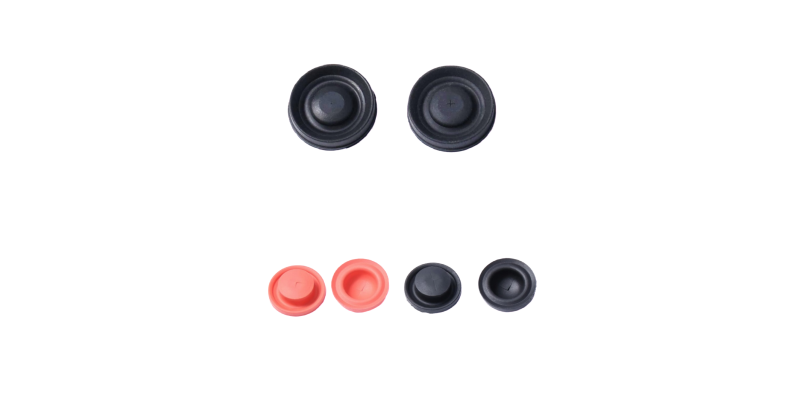
An NBR valve, also known as a nitrile butadiene rubber valve, is manufactured from high-performance nitrile rubber (NBR)—a copolymer of acrylonitrile and butadiene. This flexible one-way dispensing component is designed to provide precise flow control, reliable sealing, and leak-proof dispensing performance for liquid and semi-liquid products in squeeze packaging systems.
During squeezing, the internal slit cut opens under pressure, allowing cosmetic products to flow smoothly. When pressure is released, the valve automatically closes to create a reliable seal.
Compared with standard silicone valves, NBR rubber valves provide enhanced resistance to oils, greases, solvents, and hydrocarbon-based media, making them particularly suitable for cosmetic applications containing oil-based ingredients.
NBR material inherently resists oils, greases, lotions, and other hydrocarbon-based substances, ensuring the slit remains functional and leak-proof over time. Unlike silicone, which may swell or lose elasticity when exposed to oils, NBR valves maintain dimensional stability and sealing performance.
The precision-designed NBR valve structure provides consistent product flow, allowing consumers to easily dispense creams, lotions, and gels with minimal squeezing force.
It helps reduce product residue inside the package and improves the overall user experience.
The self-closing NBR valve automatically seals after dispensing, effectively preventing:
Product leakage
Dripping
Air backflow
External contamination
This helps maintain clean packaging and improves product shelf life.
Manufactured from high-performance nitrile rubber (NBR), the valve offers excellent resistance to oils and oil-based cosmetic ingredients. This makes it suitable for skincare and personal care products containing silicone oils, essential oils, emollients, and other oily components.
Its stable material properties help ensure:
Reliable sealing performance
Consistent dispensing control
Reduced material swelling or degradation caused by oil exposure
Long-term durability during repeated product usage
The NBR valve is an ideal solution for cosmetic squeeze packaging applications where oil resistance and dispensing reliability are required.
The NBR valve is optimized for thick cosmetic products such as creams, gels, and lotions.
Customized slit designs and hardness options are available to achieve different dispensing forces and flow rates.
NBR material maintains excellent flexibility and sealing performance after repeated squeezing cycles. It exhibits strong mechanical strength and resistance to wear, ensuring reliable operation throughout the product usage period.
Hopewell provides customized NBR valve solutions, including:
valve diameter
slit shape
slit size
material hardness
color
packaging compatibility
Our engineering team can optimize valve performance according to your cosmetic formula and bottle design.
Compared with traditional dispensing openings, NBR rubber valves provide:
✔ Better oil resistance than standard silicone valves
✔ Excellent leakage prevention
✔ Cleaner dispensing experience
✔ Reduced product waste
✔ Improved packaging hygiene
✔ Durable mechanical performance
✔ Cost-effective solution for oil-based formulas
✔ Compatibility with oil-based cosmetic formulations
How to Use
If you would like to learn how to use the cross slit NBR valve, please click the link below for detailed instructions:
Manufacturing Process
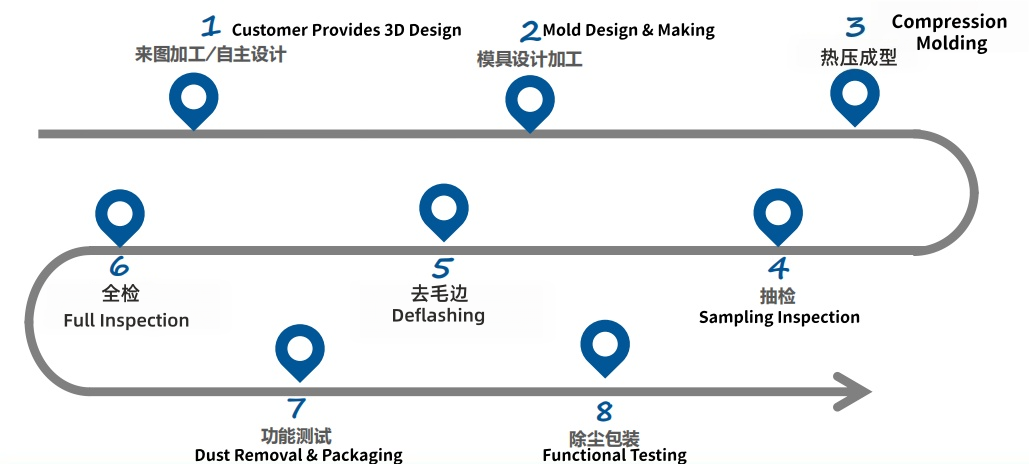
Customer Provides 3D Design → Mold Design & Making → Injection Molding → Sampling Inspection → Deflashing → Full Inspection → Functional Testing → Dust Removal & Packaging
With extensive experience in rubber component manufacturing, Hopewell specializes in the development and production of high-performance NBR valves for cosmetic packaging, personal care products, and other demanding dispensing applications.
Our expertise in NBR valve manufacturing enables us to deliver dispensing solutions with:
Excellent oil resistance against cosmetic ingredients
Stable opening and closing performance
Reliable leak-proof sealing capability
Consistent liquid flow control
Long-term durability under repeated dispensing cycles
From material selection and product design evaluation to tooling development and mass production, Hopewell provides complete custom NBR valve solutions tailored to different cosmetic dispensing requirements.
The performance of an NBR valve depends on material consistency, mold precision, and manufacturing control. Hopewell utilizes advanced injection molding technologies to ensure stable valve performance and consistent production quality.
Our manufacturing capabilities include:
Precision injection molding process
Stable valve structure and dimensional control
Optimized valve wall thickness design
Excellent elastic recovery performance
Reduced dimensional variation during mass production
These advantages ensure smooth cosmetic liquid dispensing, reliable sealing performance, and consistent valve operation throughout the product lifecycle.
Different cosmetic formulations require different dispensing forces, flow rates, and sealing performance. Hopewell provides customized NBR valve solutions based on specific product and packaging requirements.
Customization options include:
Valve size and structure
Slit design and opening pressure
Hardness selection
Flow rate optimization
Material grade selection
Color and appearance customization
Our engineering team works closely with customers from initial concept development and prototype testing to tooling production and final mass manufacturing.
A high-performance cosmetic dispensing valve requires accurate tooling design and optimized manufacturing processes.
Hopewell provides comprehensive engineering support, including:
NBR valve mold design and development
Precision mold machining
Product structure optimization
Prototype verification
Dispensing performance improvement
Our in-house engineering capabilities help shorten product development cycles while improving valve reliability and production consistency.
Hopewell applies strict quality management throughout the entire manufacturing process to ensure every NBR valve meets customer specifications and functional requirements.
Quality inspection includes:
Incoming NBR material inspection
Mold verification
Dimensional accuracy inspection
Appearance inspection
Elasticity and recovery testing
Leakage and sealing performance testing
Dispensing function testing
Comprehensive quality control ensures stable performance for cosmetic packaging applications requiring high reliability and cleanliness.
Hopewell supports both prototype development and large-scale production of NBR valves for cosmetic dispensing applications.
Our production capabilities include:
Prototype validation
Small-batch production
High-volume manufacturing
Customized packaging solutions
Stable global delivery management
Whether for skincare bottles, cosmetic squeeze packaging, lotion containers, or other personal care dispensing systems, Hopewell provides reliable NBR valve manufacturing support for global customers.
By combining NBR material expertise, precision molding technology, and customized engineering capabilities, Hopewell delivers reliable NBR valve solutions for cosmetic brands and packaging manufacturers worldwide.
Our valves are designed to provide:
Smooth and controlled liquid dispensing
Leak-proof and anti-drip performance
Excellent resistance to oils and cosmetic chemicals
Improved packaging hygiene
Enhanced consumer dispensing experience
From product design and mold development to mass production and quality inspection, Hopewell helps customers develop high-performance one-way NBR valves for modern cosmetic packaging applications.
Packaging
Our leak proof NBR valves are packed in clean polybags and export cartons to ensure hygiene and safety during transit. Custom packaging and palletization are available for bulk orders.
Item Name | PCS/Bag/Carton | Carton Size | N.W. | G.W. | Carton/Pallet | Carton/20ft HC | Carton/40ft HC |
NBR valves | 70,000 pcs/ carton | 41*31*26cm | 8kg | 9kg | 48 cartons | 430 cartons | 965 cartons |
FAQ
1
Are you a manufacturer or trading company of NBR valve?
We are a professional manufacturer specializing in spill proof NBR valves, with in-house mold design and mold making department.
2
Can I get free samples of food grade NBR valve?
Yes. Free samples are available for evaluation, shipping costs will be charged.
3
What is your MOQ of NBR valve?
Our MOQ is 50,000 pcs/lot.
4
Can you customize the size and shape of NBR valve?
Yes. We offer full customization, including valve diameter, slit shape, slit size, hardness, and coating options, to meet your specific product requirements and packaging needs.
5
Are your self sealing NBR valve food safe?
Yes. Our leak proof NBR valve are made from food-grade liquid silicone materials. They comply with FDA and LFGB standards and meet European food contact material regulations.
6
Can I visit your factory?
Absolutely! You are warmly welcome to visit our factory.
Navigation
Get in Touch
Mob.: +86 151 1847 9234
E-mail: rosie@siliconinjection.com
Skype: rosie@siliconinjection.com
WhatsApp: +86 151 1847 9234